3 Point Internal Micrometer in Saudi Arabia
- ABOUT PRODUCT
3 Point Internal Micrometer
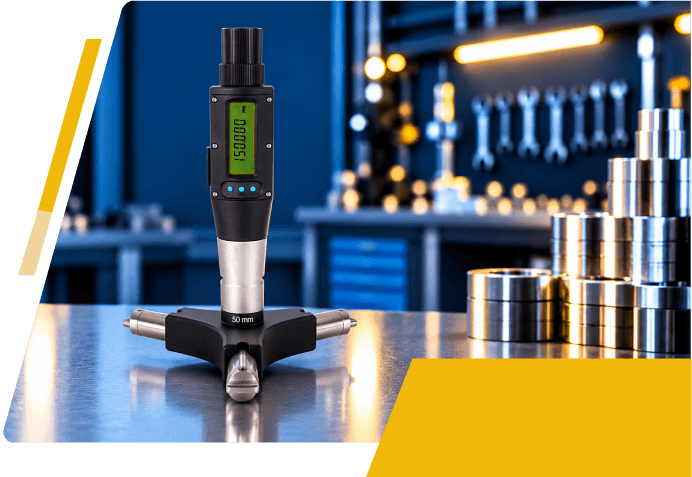
A 3 point internal micrometer reads a bore through three probes placed 120° apart. That layout centres the instrument in the hole and picks up polygonal deformation, such as the out-of-round shape that 3-jaw chucks or collets can leave, which a two-point tool can average out. Microtest builds its internal micrometers on a spindle-driven system instead of a cone system, so wear spreads evenly and is compensated linearly during routine adjustment. Repeatability is ±1–2 µm up to Ø400 mm, and ranges run from Ø30 to 1,150 mm.
3 Point Internal Micrometer
- Why Choose Us
Why Choose 3 Point Internal Micrometers?
Automatic Bore Centring
Probes spaced at 120° centre the instrument in bores.
Polygon Error Detection
Picks up polygonal deformation two-point tools may average out.
Operator Independent Repeatability
Repeatability of ±1–2 µm holds up to Ø400 mm.
Replaces Several Instruments
Can replace two to six instruments, depending on size.
- APPLICATIONS
Where 3 Point Internal Micrometers Are Used
- Machine & Tool Manufacturing
- Automotive Manufacturing
- Aviation & Aerospace
- Quality Control & Inspection
- Gear Manufacturing
- Pumps & Compressors
- Oil & Gas
- Heavy Engineering
- Power Plants
- Mining
CONTACT NOW
+971 56 744 6445
contact@egmicrotest.com
Frequently Asked Questions
It is a precision micrometer, also called an inside micrometer, that checks a bore with three probes set 120° apart. The probes centre it in the hole, so the reading does not depend on how it is held.
A two-point device uses probes 180° apart and often records only an average value, so a bore with a polygon error can look round. A three-point instrument centres itself and picks that error up. It is also easier to handle, because rod and swing systems need the operator to stabilise the instrument in two axes.
Polygonal deformation, which 3-jaw chucks or collets can cause during bore machining. Measuring in different positions gives the difference between the largest and smallest diameter.
In a cone system the probes touch the cone along a line, which causes local, non-linear wear and limits measuring range and accuracy. The Microtest spindle system has a large contact surface on the thread flanks, so wear is minimal and is compensated linearly during routine adjustment.
The bevel gear system keeps the measuring pressure constant, giving operator-independent repeatability of ±1–2 µm up to Ø400 mm.
The Microtest system compensates temperature-related expansion errors, so near-laboratory accuracy can be reached even away from the nominal 20 °C. All contact points are insulated to reduce heat transfer from the user’s hand.
They are used to check bore diameters against a tolerance in production and inspection work.